Miller's rule of thumb is that each 0.001 inch of material thickness needs 1 amp of output, so 1/8-inch (0.125 in) steel needs about 125 amps for a single pass. Choose a wire size whose range covers that current (.030 in for 40 to 145 A, .035 in for 50 to 180 A), set wire speed with Miller's multiplier for that wire, then fine-tune voltage until the arc is crisp.
The rule and where it comes from
Miller's guide to setting MIG parameters puts it plainly: material thickness determines amperage, and each 0.001 inch of thickness requires 1 amp of output. Its own example: 0.125-inch material needs 125 amps. The rule is a starting point for welding steel with solid wire in a single pass; Miller notes that joint design, position and other variables move the real setting.
The rule explains why a machine's maximum amperage and the thickest steel its maker claims are linked. A 140-amp machine reaches the current for roughly 1/8 to 9/64 inch in one pass by this rule; makers who claim more, often 1/4 inch, usually mean multiple passes or flux-core wire, and their listings sometimes say so.
Common thicknesses
| Thickness | Decimal | Starting amps | MIG wire that covers it (Miller) |
|---|---|---|---|
| 22 gauge | about 0.030 in | about 30 A | .023 in |
| 18 gauge | about 0.048 in | about 48 A | .023 or .030 in |
| 16 gauge | about 0.060 in | about 60 A | .023, .030 or .035 in |
| 14 gauge | about 0.075 in | about 75 A | .023 to .045 in |
| 1/8 in | 0.125 in | 125 A | .023, .030, .035 or .045 in |
| 3/16 in | 0.188 in | about 188 A | .045 in |
| 1/4 in | 0.250 in | 250 A | .045 in (top of its range) |
Gauge decimals vary slightly between steel tables; the decimal is what the rule uses. Above about 1/4 inch, a single pass at the rule's current is beyond most home-shop machines, and the job becomes a multi-pass weld with bevelled edges.
Picking the wire size
Miller lists the useful current range of each solid wire size: .023 inch for 30 to 130 amps, .030 inch for 40 to 145 amps, .035 inch for 50 to 180 amps, and .045 inch for 75 to 250 amps. The ranges overlap, so Miller suggests choosing a size that works for the thicknesses you weld most often, which saves changing spools and drive rolls.
For a 120-volt machine welding sheet metal and light brackets, .030 inch covers most of the range. For a 240-volt machine welding 3/16 to 1/4 inch, .035 or .045 inch suits it better. Each machine's maker states the wire sizes its drive rolls take; our product pages show them.
Setting wire feed speed
On machines that set wire feed speed rather than amps, Miller gives multipliers to turn the target amperage into inches per minute: 3.5 for .023 inch wire, 2 for .030, 1.6 for .035 and 1 for .045. With 1/8-inch steel at 125 amps, that's about 437 ipm with .023 wire, 250 ipm with .030, 200 ipm with .035 or 125 ipm with .045.
Then set voltage. Miller's advice: if the arc stubs into the workpiece, increase voltage; if it's erratic and burns back at the tip, reduce it. Too much voltage gives a turbulent pool and inconsistent penetration; too little gives poor starts, spatter and a tall, convex bead.
What makers state, and what to read next to it
Compare the rule's current with a machine's stated output, then look at its duty cycle at that current. A machine that reaches 200 amps but is rated for 20% duty there can weld only about 2 minutes in every 10 at full output. Our duty cycle calculator does that check.
| Machine | Output (maker) | Max steel (maker) | Duty cycle (maker) |
|---|---|---|---|
| Lincoln Electric K5387-9 MIG Welder | 90 Amp | Not stated | 30% duty cycle at 90 Amp |
| ESAB ROGUE EM125 MIG Welder | 125 amps | Not stated | Not stated |
| Weldpro 155 Multi-Process Welder | 155 Amp | up to 1/4" steel | Not stated |
| Weldpro 155GD Multi-Process Welder | 155 Amp | Not stated | Not stated |
| Miller 951846 Multi-Process Welder | 235 Amp | Not stated | Not stated |
| ESAB Rebel EMP 215ic Multi-Process Welder | 5-240a | Not stated | Not stated |
A worked example
You're building a trailer frame from 3/16-inch angle. The rule says about 188 amps for a single pass; Miller's table points to .045-inch wire, or .035 inch near the top of its range. A 140-amp 120-volt machine can't reach that current in one pass; a 200-amp 240-volt machine can, and its duty cycle at 190 amps or so decides how long each bead can be. The amperage selector lists machines whose stated output reaches your number, closest first.
Machines in these notes
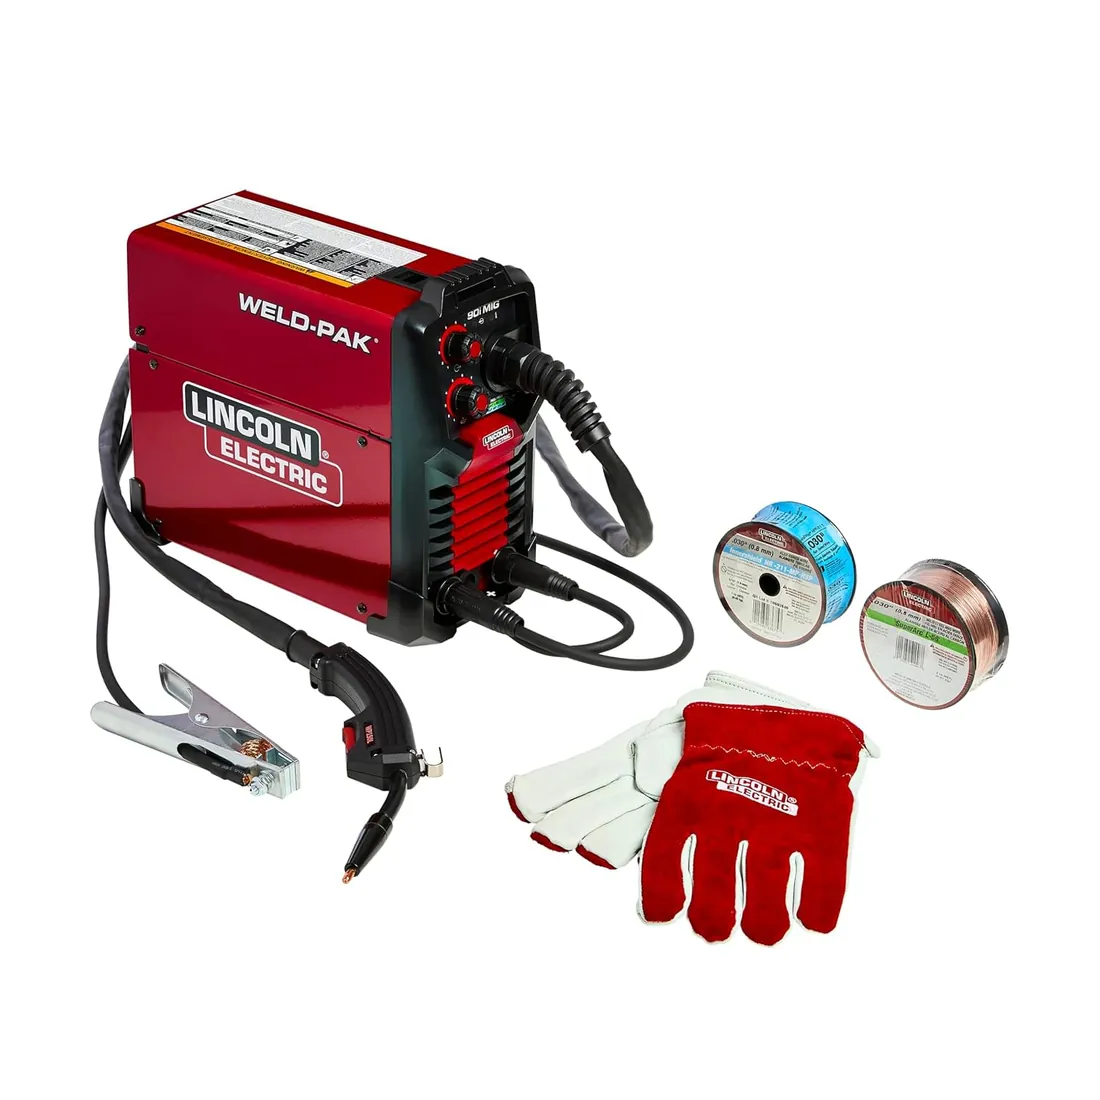
Lincoln Electric K5387-9 MIG Welder
90 A · 120 V
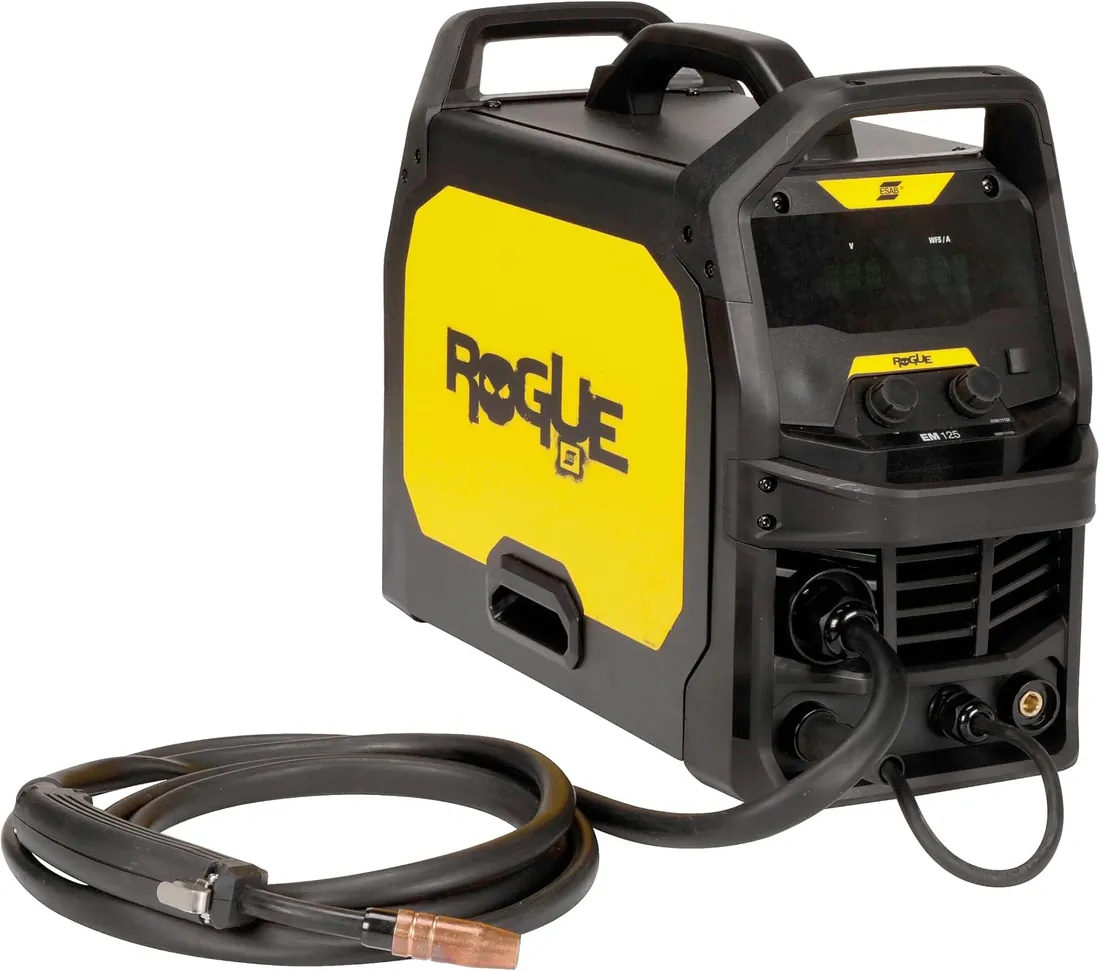
ESAB ROGUE EM125 MIG Welder
125 A · 120 V
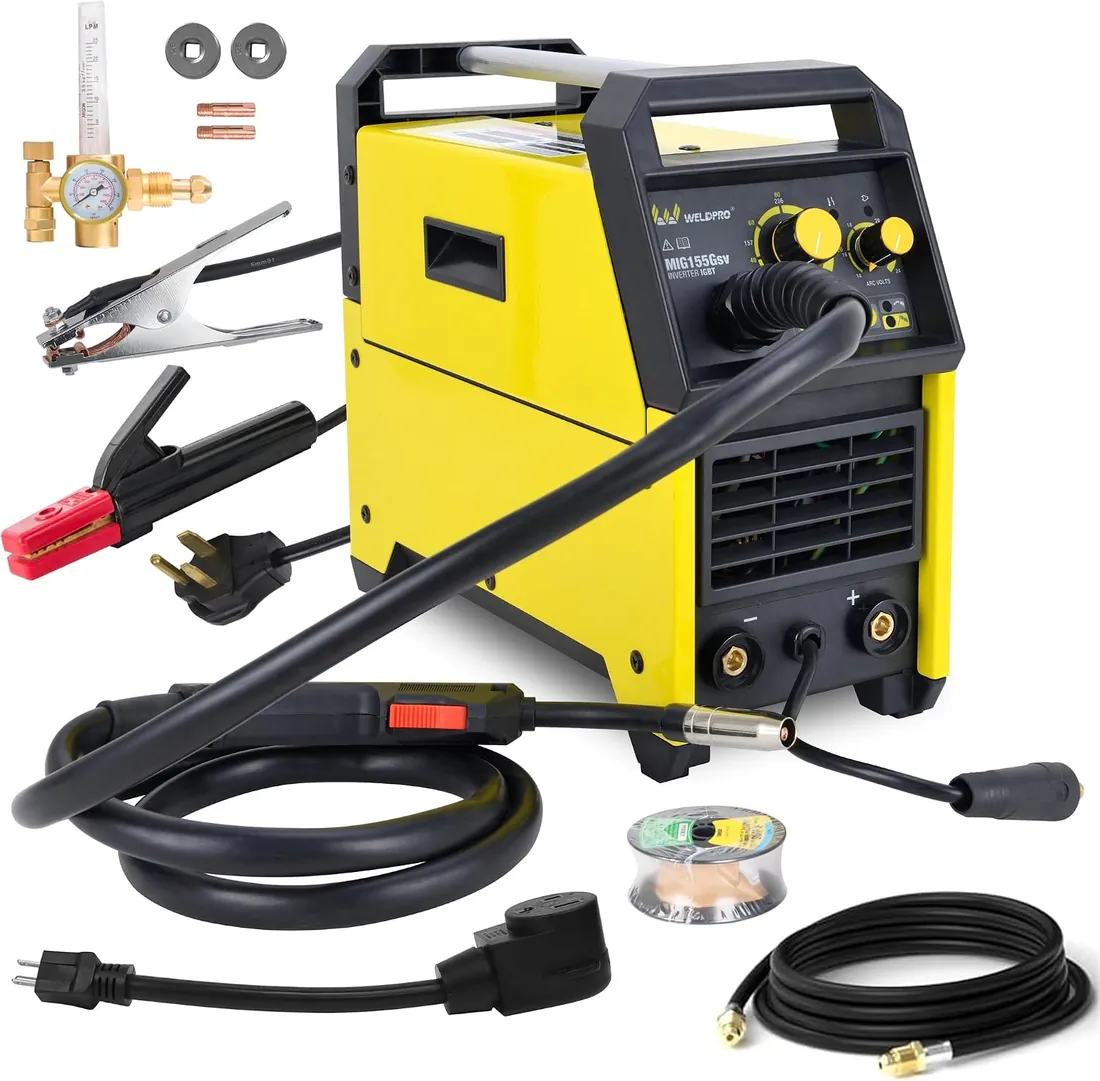
Weldpro 155 Multi-Process Welder
155 A · 220 V
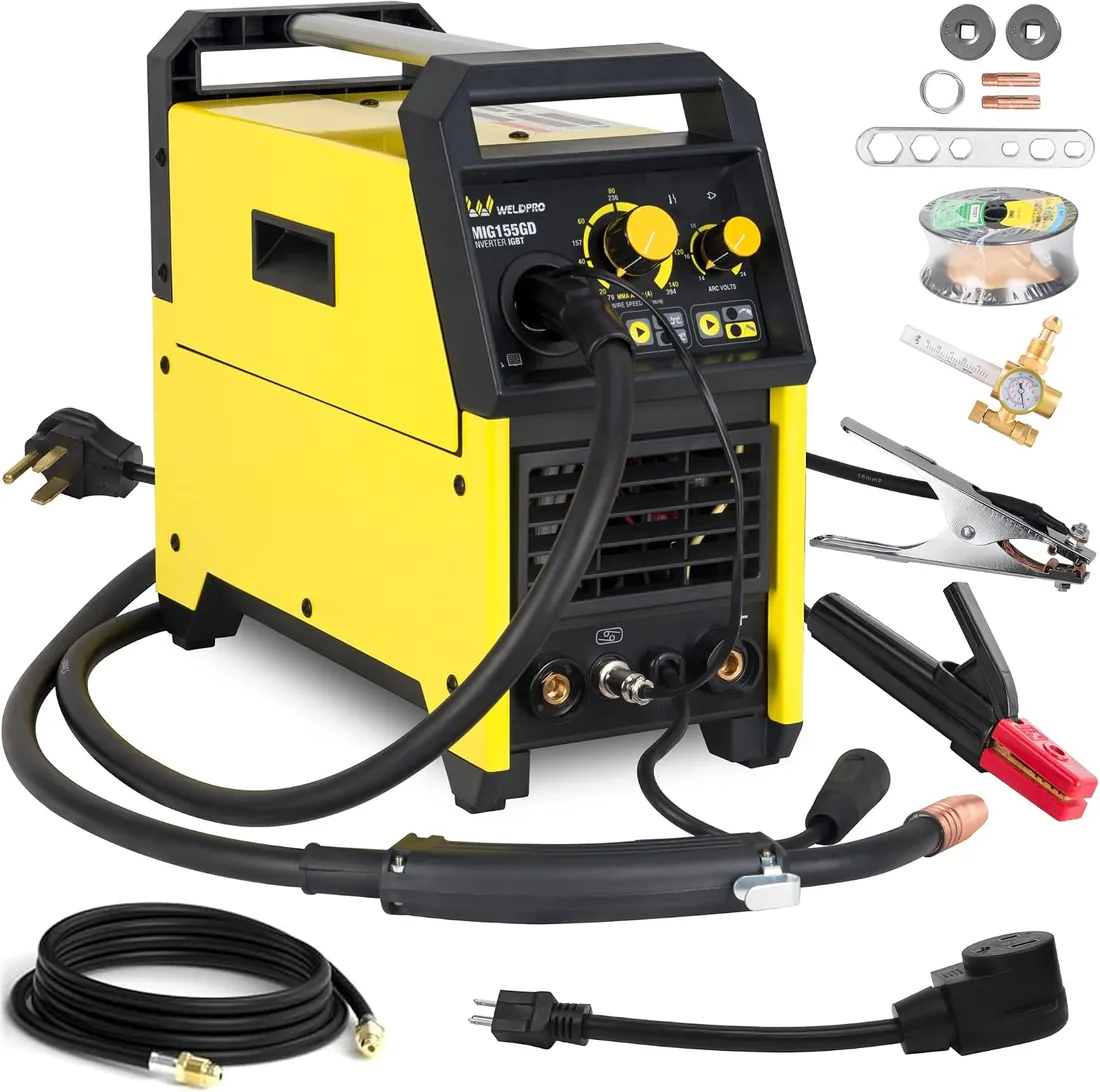
Weldpro 155GD Multi-Process Welder
155 A · 220 V
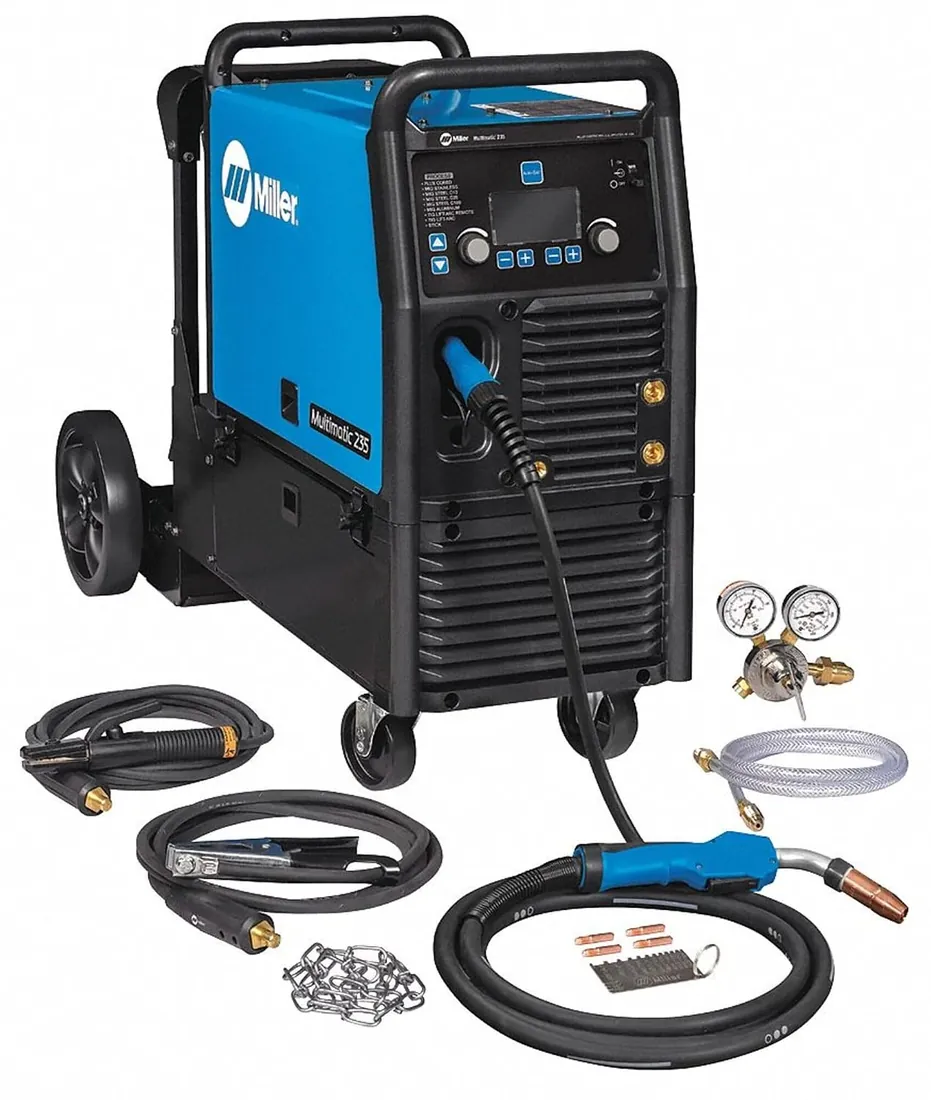
Miller 951846 Multi-Process Welder
235 A · 240 V
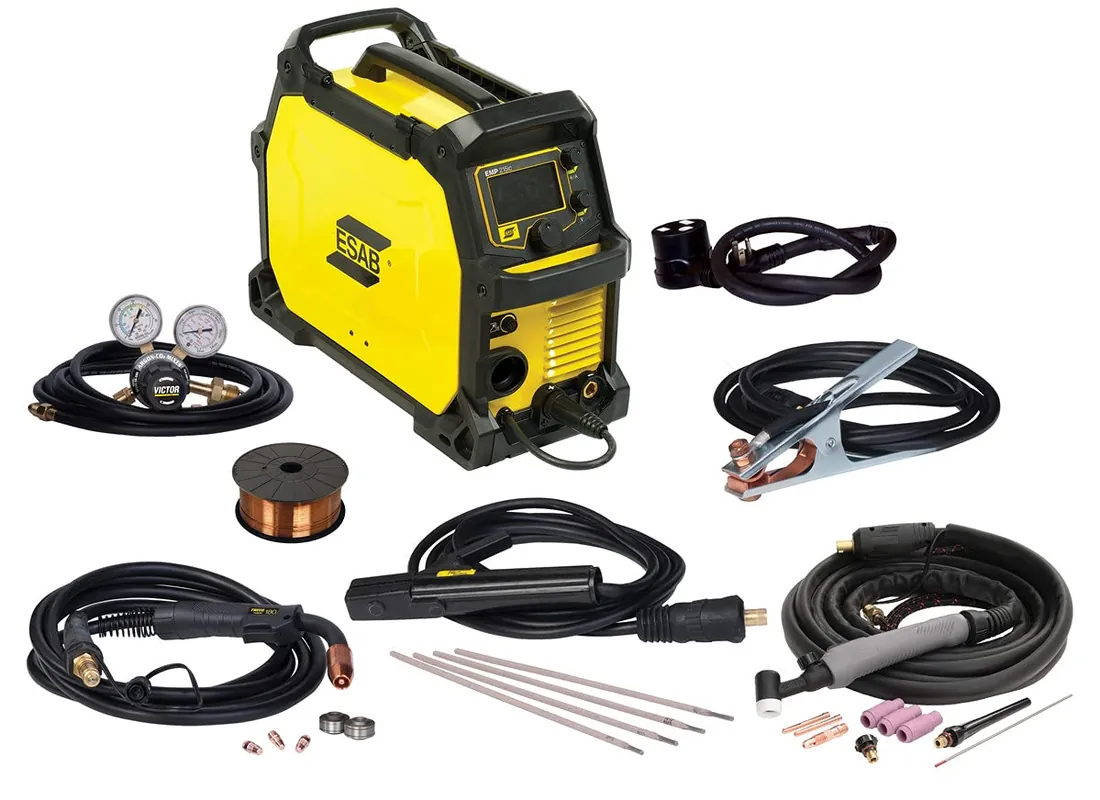
ESAB Rebel EMP 215ic Multi-Process Welder
240 A